Modellbahn Keks
Welcome!
Our cookies offer you a fast, relaxed and full-featured shopping experience. Some are necessary to operate the website and its functions. Others help us to improve our services. If you agree to this, simply consent to the use of cookies for preferences, statistics and marketing by clicking on "OK". Alternatively, you can deactivate individual cookies under "Customise cookies" or all cookies, except those required for the function of our website, under "Reject all".
Anycubic Photon Mono 4 Ultra Resin 3D Printer
Filament or resin?

FDM or Resin for Model Railways and Model Making?

FDM is often a practical starting point for buildings, terrain shapes and workshop aids. Resin excels at fine figures, ornaments and small vehicle details. The best process depends on your component, together with the material, post-processing and workspace.

The decision starts with the model

What does your print need to do?

FDM or resin for model railways and model making? Start by comparing the smallest important detail, the component's size and the loads it will face. A tunnel lining needs different properties from an engine driver's face. One process does not have to handle every task on your layout.

FDM is often suitable when …

… you want to make larger building shells, retaining walls, simple wagon loads or brackets. Filament printing offers many material options for these tasks and a workflow without a resin vat. Allow for visible extrusion lines and sanding where necessary.

Resin is often suitable when …

… faces, small rivets, delicate window frames or ornaments are your focus. Plan a suitable resin workspace and the specified post-processing steps. Despite the high level of detail, thin parts still need careful design.

If you do not have a suitable resin workspace, external printing services are an alternative. You can have fine detailing parts printed and produce larger components yourself using filament. The 3D printing knowledge hub brings materials, software and model railway projects together.

Two routes to a three-dimensional component

How filament and resin printing work

FDM or FFF

A print head melts a plastic filament and deposits it as a thin line. Outer walls, top and bottom surfaces, and a planned internal structure form the model layer by layer. Here, FDM and FFF describe the same basic process. PLA and PETG are examples of different filament materials; their properties and print profiles are not interchangeable.

Resin, SLA, MSLA and DLP

Resin is a light-sensitive liquid. Resin printing cures it selectively, layer by layer. Conventional laser SLA traces each layer with a laser, MSLA uses an LCD mask and DLP uses a projector. These processes differ technically, but all belong to resin printing. A bottle of resin must be compatible with the printer and the intended exposure profile.

For both processes, a slicer converts the digital model into print layers. An existing file is not automatically ready to print: orientation, wall thicknesses, supports and later assembly must suit the chosen process.

Consider strengths and workload together

The main differences at a glance

Comparing FDM and resin for model making
Criterion FDM / filament Resin
Fine detail The nozzle, line width and orientation limit small contours. Often advantageous for small faces, rivets and ornaments.
Surface finish Extrusion lines are often visible; allow for finishing visible surfaces. Often finer surfaces, although layer lines and support marks can still occur.
Build volume Large building components are a typical application; check printer dimensions. The build area, supports and cleaning space also limit the project.
Strength Consider the material, wall structure and loads acting across layer interfaces. Resin type and post-curing are decisive; do not equate standard resin with tough resin.
Post-processing Cool, release and remove supports; sand and prime as required. Wash, dry and post-cure according to the manufacturer's instructions; remove supports.
Odour and workspace Emissions can occur even with little noticeable odour; plan ventilation. Liquid resin and cleaning fluids require protection and an organised workflow.
Costs and time Account for material, toolpaths, failed prints and surface finishing. Include material, cleaning, consumables and post-processing time.

This comparison applies technical fundamentals to typical model-making tasks. It does not document our own comparative test prints. A sample containing the details you actually need is particularly helpful for a well-founded buying decision.

Six typical tasks

From station buildings to signals

Choose the process for the specific component
Project Suggested approach What matters
Buildings and façades FDM for building shells, resin for fine decorative parts. Window bars, masonry texture and visible glue joints.
Bridges FDM for larger girders, with other materials for fine railings. Check loads, deflection and secure track support separately.
Figures Resin for small faces, hands and folds in clothing. Keep support contact points away from faces and prominently visible body surfaces.
Signals and detailing parts Resin for fine signal heads; also consider metal for long, thin posts. Cable routing, risk of breakage and access for assembly.
Vehicle bodies Resin for fine details, FDM for larger shapes or prototypes. Warping, wall thickness, window openings and fit to the chassis.
Workshop aids FDM for brackets, organiser inserts and assembly jigs. Load direction, temperature and sufficiently strong fixings.

The same division applies to other areas of model making: architectural models benefit from well-planned subassemblies, and small diorama figures from fine surfaces. Load-bearing and moving parts in RC models require separate strength checks. A printed shape is not proof of its suitability in service.

Plan combinations of materials deliberately. Wire railings, etched mesh or a laser-cut façade may be a better solution than an extremely fragile print. When scratch-building buildings , established construction methods and bespoke printed parts can work well together.

Smaller scales, different requirements

What changes from T and Z to garden railways

In T, Z and N, small scenic details quickly become challenging. Resin is worth considering for figures, delicate frames and lettering. Supporting structures and simple terrain forms remain sensible FDM projects at these scales too. Scale alone therefore does not determine the process.

In TT and H0, a combination often makes sense: building shells from filament and fine detailing parts from resin. In OO, S, 0 and 1, build volume and designs that split into sections become more important. Larger models still contain small details that may justify making them separately.

II, IIm and garden railways also require UV, temperature and moisture resistance. These properties must be documented for the specific material. For detail size, H0e, H0m, TTm, Nm, 0e and 0m follow the scale ratio of their parent scale. Further relationships are explained in the scale and gauge comparison .

Resolution is not the same as dimensional accuracy

Assess detail, surface finish and strength properly

Thinner layers do not solve every problem

With FDM, layer height mainly affects vertical stepping. For small contours in the printing plane, nozzle diameter and line width are among the important factors. A suitable smaller nozzle can help, but requires appropriate settings and more print time. Check the slicer preview before starting a large model.

More display pixels do not guarantee quality

In MSLA printing, display size and pixel pitch must be considered together. Exposure, resin, supports and orientation also influence the result. A high nominal resolution does not guarantee a correctly sized hole or a straight locomotive side panel. Test push-fit connections and recesses on a small sample.

The loads in use determine material selection

With FDM, bonds between layers can be vulnerable to forces acting in an unfavourable direction. Wall thickness, perimeters and orientation are therefore as important as infill. With resin, rigid standard formulations and tougher specialist resins differ considerably. Terms such as “Tough” or “ABS-like” do not replace material data or testing the finished component.

For long, thin ladders or railings, compare metal alternatives regardless of the printing process. For larger surfaces, splitting the design, adding reinforcement and carefully positioning glue joints can make warping easier to manage. Design for the finished model and its assembly, not just an attractive view on screen.

The work continues after printing

From the print bed to a paint-ready model

A typical FDM workflow

  1. Check and orient the file, then prepare it with a suitable filament profile.
  2. Check the first layer and run the print.
  3. Let the component cool and release it from the plate as instructed.
  4. Remove supports and burrs; finish visible surfaces as needed.
  5. Check the fit, clean and apply a primer suited to the material.

A typical resin workflow

  1. Orient the component and plan supports and, where necessary, drain holes.
  2. Print with a suitable resin profile and allow the part to drain in a controlled way.
  3. Wash according to the material instructions and allow to dry completely.
  4. Remove supports at the recommended stage and post-cure as specified.
  5. Check support contact points and prime the prepared model.

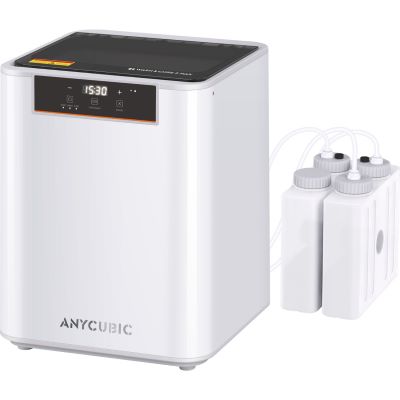
A wash-and-cure station organises parts of the resin workflow. The washing fluid, duration and post-curing must still suit the material. In hollow resin models, liquid resin and cleaning fluid must drain reliably; the interior must also be accessible and correctly post-processed. Avoid unplanned sealed cavities.

Sanding and thick coats of primer can obscure detail. Work on a sample first and position support contact points on less visible surfaces wherever possible. Advice on weathering buildings then helps printed and traditional components blend visually.

Compare the finished result

What really affects print time and total costs

With FDM, the nozzle traces the toolpaths for individual parts. More components therefore often mean longer print times. With MSLA and DLP, an entire layer is exposed together. Several miniatures of similar height can therefore use the build plate efficiently. This does not apply in the same way to laser SLA; layer count, movements, resin profile and geometry also affect the process.

Always compare the time needed to obtain a usable model. A quick resin print followed by washing and post-curing may require more hands-on work than a simple FDM part. Conversely, extensive sanding of a visible FDM surface can use up the apparent time saving. A blanket statement that “resin is faster” is therefore of little help.

Cost calculations need to include material for supports and failed prints, electricity, consumables and post-processing. Resin also requires cleaning fluids and protective equipment; FDM may involve material drying and multicolour purge waste. Compare current prices for filament and resin based on the amount actually used. A price per kilogram alone tells you little about the cost of a finished figure.

Space, ventilation and clean working practices

The workspace is part of choosing the process

FDM does not require a resin washing area, but can release particles and volatile substances. Little odour does not automatically mean low emissions. Follow the printer instructions and material guidance, and provide suitable ventilation or emission extraction. Also allow space for moving components, hot surfaces and material changes.

Handle resin carefully

Avoid contact with liquid or insufficiently cured resin. Use suitable protective gloves and eye protection as specified in the safety data sheet. Provide an organised work area with appropriate ventilation, sealable containers and dedicated tools. Cleaning fluids may introduce additional hazards, such as flammability.

Water-washable does not mean harmless: resin residues and contaminated wash water must not go down the drain. Check disposal requirements in the product information and with your local waste disposal service. An integrated printer filter does not automatically replace a suitable ventilation arrangement.

If you cannot organise these processes sensibly at home, have fine parts produced externally. A suitable workshop setup is more important than the highest possible detail resolution on a specification sheet.

One project for both processes

An H0 waiting shelter as a practical starting point

Plan the shell and details separately

The waiting shelter has a simple shell, a removable roof and a small bench. Walls and roof are suitable FDM candidates. Resin is worth considering for an ornate bench or a waiting figure. This is a planning example; adapt the dimensions and printing parameters to your own design.

Gather materials and tools

You need suitable files, compatible filament or resin, callipers, a deburring tool and an adhesive compatible with the material. Resin also requires the complete protective, washing and post-curing setup. Primer, paint and a brush complete the surface-finishing tools.

Print only the critical feature first

Test a wall with a window opening and a small section of the bench. Check visible features, mating surfaces and glue joints. Then decide which details should be reinforced in the design or made separately.

Assess again after priming

A thin test coat shows whether details remain visible and whether layer lines are distracting. Adjust the model before printing a batch. This uses less material and helps establish a repeatable workflow.

Explore relevant manufacturer ranges

Compare printers, materials and accessories within their respective systems.

From comparison to the right material

Browse the current FDM and resin range

The product list loads items from the linked categories. Search by name, colour or item number, and combine printing process, category and manufacturer filters. Check specific equipment and material compatibility on the product page.

The product list is being prepared. You can access the categories directly.

Explore all 3D Tools

Frequently asked questions about filament and resin

Is resin always better than FDM?

No. Resin is often useful for small visible details, while FDM suits larger shells and many workshop aids. Material, geometry and workflow together determine suitability. A well-designed FDM part may be the better choice for its task.

Can I print H0 figures with FDM?

In principle, yes, but faces, hands and small folds in clothing are demanding. A suitable nozzle, profile and design improve the result. If fine visible detail is essential, a resin sample is worth comparing.

Are resin parts always brittle?

No. Different resin formulations are available, including tougher and flexible variants. Material data, component geometry and correct post-processing are decisive. A very thin railing remains delicate even with a suitable resin.

Is water-washable resin safe to use in a living space without special precautions?

Water-washable describes the cleaning medium. Protective measures, ventilation and responsible disposal remain necessary. Contaminated wash water must not go down the drain. Base your decision on the complete workspace and the manufacturer's information.

Can the same STL file be printed with both processes?

The same source model can often be used. However, supports, orientation, wall thicknesses and any cavities need to be reassessed. Do not transfer prepared print data or profiles from one process to the other without checking them.

Do I need to buy both printers for a model railway layout?

No. Start with the process suited to your most frequent projects. You can have occasional specialist parts printed or make them from traditional modelling materials. A second system is worthwhile only when demand, workspace and workload justify it.

Technical fundamentals: Prusa on printing processes, layer height and perimeters, hollowing resin prints, Formlabs on resin post-processing and NIOSH on emissions and occupational safety.

Chosen your process? Plan your first model.

Combine the knowledge from the 3D printing knowledge hub with scratch-building, scenery and suitable materials.

Explore the model railway guide