Modellbahn Keks
Welcome!
Our cookies offer you a fast, relaxed and full-featured shopping experience. Some are necessary to operate the website and its functions. Others help us to improve our services. If you agree to this, simply consent to the use of cookies for preferences, statistics and marketing by clicking on "OK". Alternatively, you can deactivate individual cookies under "Customise cookies" or all cookies, except those required for the function of our website, under "Reject all".
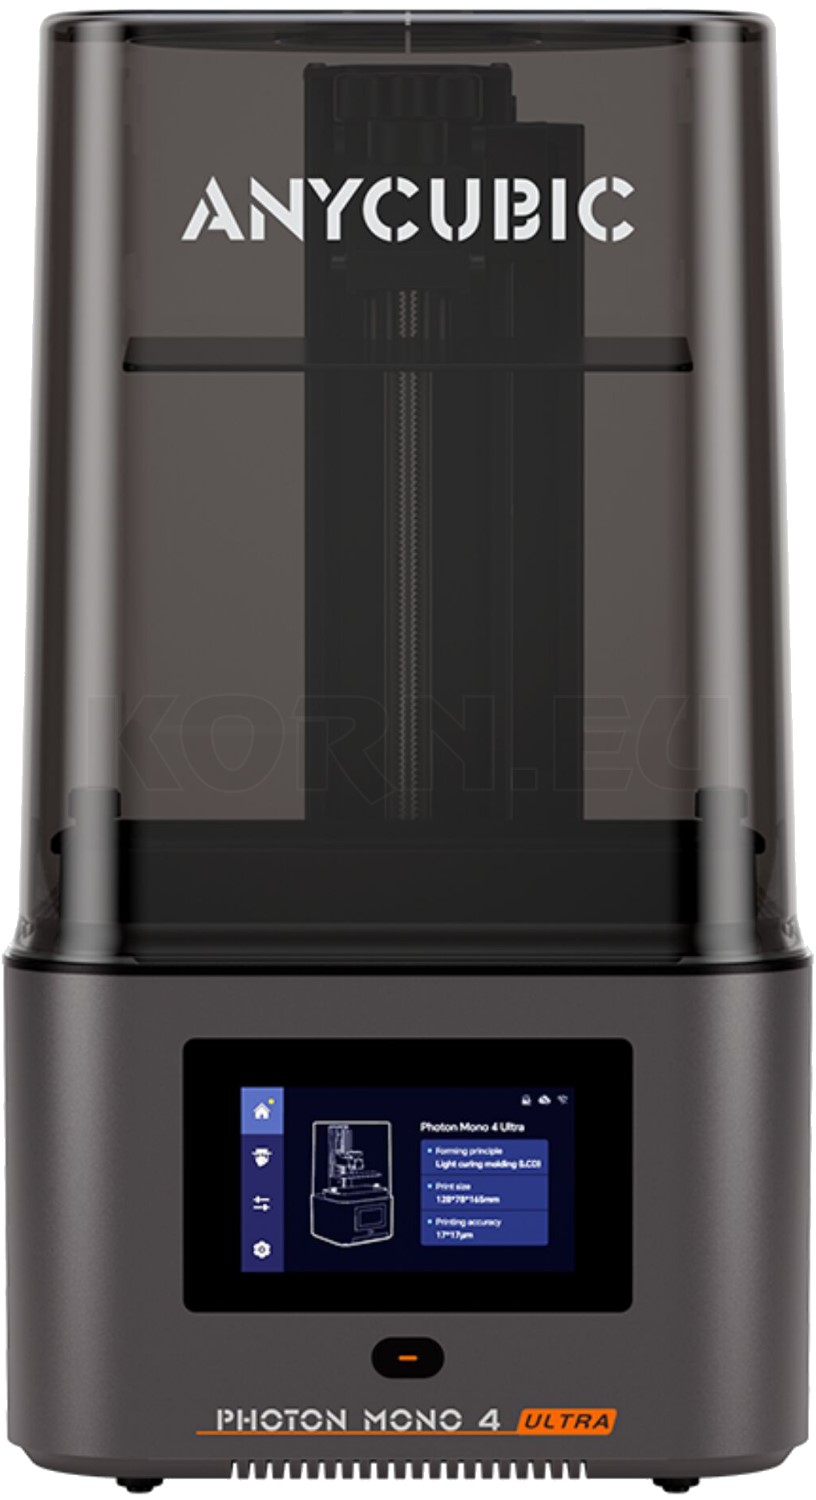
Anycubic Photon Mono 4 Ultra Resin 3D Printer for small model-making projects
Custom details for your TT layout

3D Printing for TT – Detailed Models in 1:120 Scale

FDM remains a useful choice in TT for building shells, walls and robust auxiliary parts. Fine windows, figures and vehicle details often benefit from resin. Good results come from suitable designs, controlled test prints and deliberately strengthened details.

Plan small parts carefully

Which printing process suits your TT project?

3D printing for TT: detailed models in 1:120 opens up possibilities for custom stations, workshops and vehicles. Choose the process according to the smallest important detail. A large building shell and its narrow window frames do not have to use the same printing process.

Typical TT applications and their key checks
Project Suitable approach Check before batch printing
Sheds, façades and walls FDM for broad surfaces, resin for separate decorative parts Mortar joint detail, window openings and straight gluing edges.
Benches, electrical cabinets and crates FDM for robust shapes, resin for fine outlines Legs, handles, support contact points and handling during painting.
Window frames and ventilation grilles Resin or a small FDM nozzle with adapted struts Clear gaps and strength after finishing.
Railings, ladders and handrails Resin for suitable geometries; wire or etched parts as additions Unsupported spans, weak points and mounting points.
Figures and vehicle details Resin where high detail is required Faces, hands, thin fittings and mating surfaces.
Coupling mounts and assembly jigs Choose the process and material to suit the function Dimensions, freedom of movement, strength and repeated loads.

A small enclosed object with clearly defined surfaces, such as a crate, makes a good starting point. A railing with many freestanding bars is considerably more demanding. Start with one sample and expand the project only after successful assembly.

Treat external dimensions and details separately

Scale correctly to 1:120

One full-size metre corresponds to approximately 8.33 millimetres in TT. A person 1.80 metres tall is about 15 millimetres high; a gate three metres wide becomes 25 millimetres wide. First convert the starting dimensions to the same unit and check the actual dimensions after importing.

From H0 at 1:87 to TT, the linear scaling factor is 87 ÷ 120 × 100 = 72.5 per cent. An N-scale file at 1:160 is enlarged to approximately 133.33 per cent. From Z at 1:220, it is approximately 183.33 per cent. This applies to the geometry, but does not automatically produce workable wall thicknesses or push-fit joints.

A one-millimetre-thick H0 wall becomes just 0.725 millimetres thick when reduced. An already thin strut becomes even more fragile. Adjust external dimensions and critical details separately in CAD. For these revisions, editable design files are often more useful than a heavily simplified triangle mesh.

Start with a test piece

Starting ranges for detailed TT prints

The following values are our suggested starting points for test prints, not documented print tests or universal manufacturer profiles. Use an approved profile for your printer, the specific material and the nozzle fitted. The wall thicknesses are robust design starting points for small surfaces; a long freestanding rod needs separate assessment.

Choose print settings and design strength together
Application Nozzle and layer height Starting wall thickness
FDM main structures and building parts 0.4 mm nozzle; approximately 0.12–0.16 mm layer height Approximately 1.0–1.4 mm; reinforce or divide large surfaces.
Small FDM accessories Approved 0.2 or 0.25 mm nozzle; approximately 0.08–0.12 mm Approximately 0.6–0.8 mm for small, protected walls; check toolpaths in the slicer.
Resin housings and fine accessories Start with a suitable 0.05 mm profile; compare 0.03 mm where useful Approximately 0.8–1.2 mm for small housings; plan supports, openings and post-curing.

Layer height and line width serve different purposes

Finer layers improve stepping in the Z direction. They do not automatically make a window mullion printable if it is too narrow in the printing plane. First check the preview of the actual toolpaths generated. A suitable wall thickness also depends on line width, layer height and overlap between extrusion paths.

Variable line widths, for example with Arachne in PrusaSlicer, can reproduce thin areas more effectively. Limits still apply: features that are too small may be omitted, while others are widened. Check both the strut and the opening beside it. A visible line in the preview is not proof of sufficient strength.

Fine-tune exposure and material profiles

For resin, begin with the exposure and motion settings specified for your printer and resin combination. Temperature and layer height affect the result. Overexposure can close small gaps; underexposure can cause weak or incomplete parts. Use a suitable calibration test before arranging numerous TT parts on the build plate.

For FDM, temperature, cooling and minimum layer time belong to the material profile. Very small individual parts have little time to cool. Check the profile and print sequence instead of simply increasing speed. Small nozzles also require suitable filaments; coarse particle additives are not compatible with every nozzle opening.

Delicate yet practical to assemble

Design windows, railings and vehicle parts

Deliberately strengthen window mullions

A full-size mullion 40 millimetres wide becomes only about 0.33 millimetres wide in TT. Exact scaling is not always the best construction method. Compare slightly stronger struts and larger clear openings on a small window section. Keep the visible frame slim and, where needed, reinforce it on the hidden rear face.

Separate window frames make material selection and painting easier. Clear film can provide the glazing. Allow a supporting ledge and some assembly clearance so the pane is not under stress. Assess the appearance from normal layout viewing distance too; paint can alter tiny openings more than expected.

Railings and ladders need a sound structure

A tube with a full-size diameter of 30 millimetres would have a model diameter of just 0.25 millimetres. At this size, unsupported length, material and contact during installation matter particularly. Thicken vulnerable transitions, divide long railings into sections or combine printed posts with wire. Etched parts are another option for particularly fine, flat structures.

Place support contact points where they will later be hidden or easy to finish. Avoid applying leverage to thin bars when removing supports. A broken railing often calls for a design change; a smaller layer height alone will not eliminate the weak point.

Coupling pockets are functional parts

For interchangeable coupling heads in TT and N, the MOROP recommendation NEM 355 (German PDF) describes the coupling pocket; NEM 359 is also relevant for TT. Simply scaling down an H0 pocket does not reproduce this geometry. Mounting height, guidance and space for movement must also suit the vehicle.

First test a custom part with the intended coupling head, then when pulling and pushing through the tightest curves and points you use. Check free movement, return to centre and repeated loads. Printed spring tabs and snap-fit lugs may behave differently from production parts because of their material. For a first conversion, a printed bracket with a suitable ready-made pocket is often easier to assess.

A few features make all the difference on figures

An adult TT figure is approximately one and a half centimetres tall. The face, hands and foot positions must remain recognisable within this small space. Resin often offers better possibilities than FDM here. Compact poses and fewer freestanding details make handling easier. Ready-made figures can complement a custom-printed scene.

A small project with clear checkpoints

Plan a TT electrical cabinet as a resin project

This original design example is a planning guide, not a report of a completed print test. It assumes full-size dimensions of 1.20 metres wide, 0.60 metres deep and 1.80 metres high. These become ten × five × 15 millimetres on the model. The cabinet has a suggested door outline and an open back.

Prepare materials and tools

You need a suitable resin, a compatible printer, CAD software and a slicer, callipers, suitable support-removal tools, and primer and paint compatible with the material. The workflow includes cleaning and post-curing according to the manufacturer's instructions. A separate plinth made from sheet material makes positioning easier later.

1

Define the main body and walls

Design the external dimensions and begin, for example, with a wall thickness of 0.9 millimetres. The open back provides access to the inside. Do not create a sealed cavity where liquid resin could remain trapped. A simple raised handle detail is easier for a first project than a freestanding loop.

2

Compare door details on a sample

Start with just a small section containing the door gap and handle. Compare different widths and depths instead of immediately printing a whole batch. Mark the variants clearly so you can match the best result to the correct file.

One change per comparison

Keep the material, orientation and profile the same while comparing geometry. For an exposure test, by contrast, keep the geometry unchanged.

Assess the painted sample too

Apply a thin coat of primer to a successful sample. Check that the gap and handle remain visible before making multiple copies of the complete cabinet.

3

Check orientation and supports

Orient the part so resin can drain and no enclosed suction cup forms. Place support contact points on the back or lower edge wherever possible. Check the layers for unsupported islands. A standard tilt angle is no substitute for this check.

4

Finish and install

Clean, dry and post-cure the part according to the material instructions. Remove supports in the recommended sequence, tidy the contact points and check the fit on the plinth. Paint only after the trial fit and position the cabinet clear of passing vehicles.

The same approach can be used for small junction boxes, workshop furniture and platform accessories. For the surroundings of buildings, see the guides to scratch-building buildings and designing platforms. Complete the scene with suitable building accessories.

Consider material, finishing and costs together

PLA is a useful starting point for many decorative FDM parts used indoors. PLA+ covers different manufacturers' formulations. PETG may be useful for brackets under load; fine outlines and fits still need testing. A material name does not guarantee suitability for every TT design.

With resin, detail reproduction and toughness should be assessed separately. Minimum printable wall specifications apply to particular printers, materials and test conditions. They do not guarantee that a TT railing of the same thickness will survive installation. Large, thin surfaces can also warp during printing, washing or post-curing.

Follow the manufacturer's instructions and safety data sheet, particularly regarding suitable gloves, eye protection and ventilation. Water-washable resin also requires proper cleaning and disposal; wash water containing resin must not go down the drain. Find suitable equipment in 3D accessories.

Arranging several small parts on one build plate spreads the preparation effort across them. However, check every part for supports and adequate spacing. Calculate materials, failed prints and hands-on finishing time with the 3D printing cost calculator. A full plate of untested geometry can quickly produce more waste than a single test.

Resolve faults using the smallest informative sample

  • Missing struts: check the scale and slicer preview. Adjust geometry, nozzle or line width before repeating the print unchanged.
  • Openings are closed: first compare CAD dimensions and the preview, then investigate material flow or resin exposure. Do not scale up the entire model.
  • Parts no longer fit after painting: check assembly clearance and paint layers. Keep gluing and mating surfaces clear as needed.
  • Fittings break during installation: consider support contact points, transitions and leverage. Reinforce mounting points or choose another construction method.

Keep a successful reference part together with its file version, material and profile. Compare reprints against it. This helps you spot changes without relying solely on an enlarged screen image or photographs taken under different conditions.

Explore the manufacturers' ranges

Compare printers, materials and accessories within each system.

Equipment for your TT projects

Find printers, filaments and resins

Search by product, material, colour or item number. Combine process, category and manufacturer filters. The list loads current products from the linked categories. Check printer compatibility and material properties on the product page.

The product list is being prepared. You can open the categories directly.

View all 3D tools

Frequently asked questions about 3D-printed TT models

Is FDM too coarse for TT?

Not necessarily. Building shells, walls and robust auxiliary parts are useful applications. Thin window mullions and detailed figures are more demanding. Decide based on the smallest detail you need.

Can I reduce every H0 file to 72.5 per cent?

This converts the external dimensions to 1:120, provided the source file is actually 1:87. Wall thicknesses, holes, supports and coupling geometries must then be checked separately.

Which layer height is suitable for TT figures?

A suitable resin profile with 0.05 mm layers is a starting point. If needed, compare 0.03 mm with exposure adjusted for it. Finer layers do not replace good modelling and support placement.

What minimum wall thickness is safe?

There is no universal value. Material, surface area, unsupported length, orientation and subsequent loads determine the strength margin needed. Use the table as a design guide and test a representative sample.

Can I print my own TT couplings?

This is a demanding functional project. Check standard geometry, mounting height, freedom of movement and material behaviour. A print that looks right does not yet confirm reliable operation on the layout.

Where can I find suitable STL files for TT?

Search for TT, 1:120 and the specific part. Check dimensions, file previews, printing guidance and permitted use. Missing wall thicknesses or unclear units should be corrected before printing.

Technical background: MOROP standards index (including NEM 010, 355 and 359), Prusa on variable line widths, Prusa on layers and wall thicknesses, Anycubic on resin parameters and Formlabs on printer-specific detail limits. The project dimensions and starting ranges are our own planning examples.

Add your own details to your TT layout

Combine the 3D printing knowledge hub with traditional model making and develop your next scene from a successful sample.

Explore the model railway guide